
Centrifugal Pumps in Putnam County
Choosing the Correct Drum Pump in Putnam County
When selecting the ideal drum pump for a specific use, there are several factors that should be taken into account. These factors include:
- Compatibility with the medium being transferred: Different models of drum pumps are specifically designed to handle different types of liquids. It is crucial to select the pump that is compatible with the type of liquid you need transported, as some liquids or chemicals can be too abrasive or viscous to work with certain models.
- Power source: Choose a pump that will meet the demands of your application and the type of power source you have available.
- Safety considerations: Pick a pump that complies with applicable safety regulations and is suitable for the unique dangers prevalent in your application. Make sure the pump is explosion-proof, for instance, if you are transporting explosive liquids.
- Price: Establish your spending limit and select a pump that satisfies your requirements at a cost you are comfortable paying.
- Volume and flow rate: Consider both the volume and flow rate of the liquid you need to move. Ensure that the drum pump you select has a flow rate that meets your requirements.
- Size and weight: Take into account the size and weight of both the pump and the drum or other container from which you will be transferring the liquid. Verify that the pump can fit inside the drum and is not too heavy to handle.
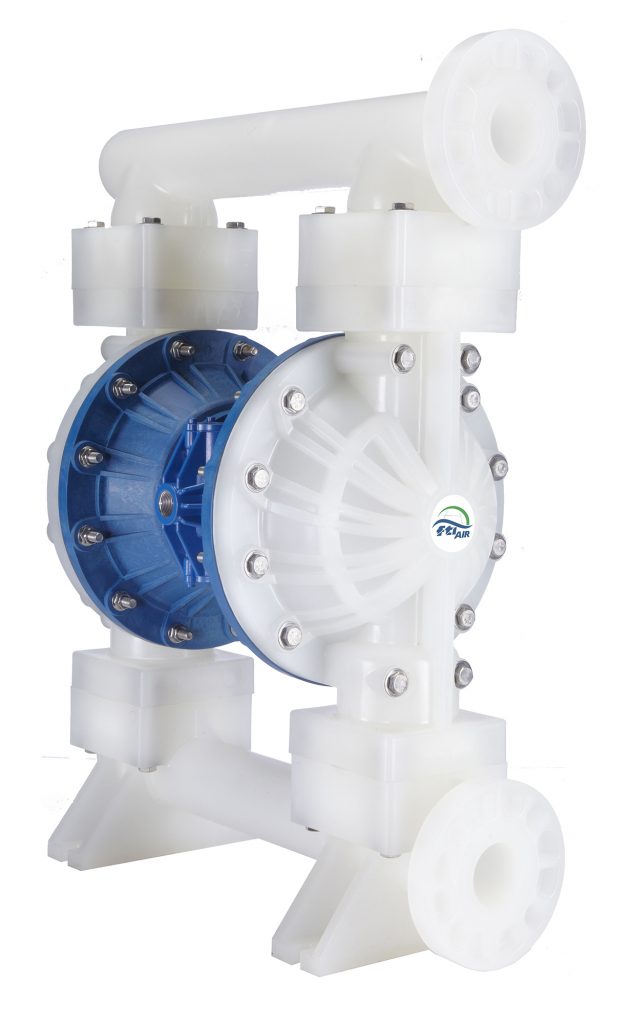
Putnam County Air-Operated Diaphragm Chemical Pump Designs & Their Advantages
Fluid-handling devices that employ air pressure to transfer fluids include air operated diaphragm chemical pumps. They are available in several designs, including single- and double-diaphragm models, ball valve layouts, and nonmetallic wetted component setups. These pumps are adaptable and reasonably priced. They can tolerate caustic or abrasive fluids, have high flow rates, and can prime themselves.
They can be used even if the liquid levels change because they are self-priming and can run dry without causing damage. Additionally, they require relatively little maintenance and can deliver a constant flow rate. Last but not least, because these pumps are air-operated, they are simple to install and use a small amount of electricity.
Drum Pumps in Putnam,
For transfering and dispensing fluids.
Putnam County Drum Pump Accessories
- SPILLSTOP - Fully pneumatic system safely captures leaked product due to diaphragm failure and automatically shuts down failed pumps to eliminate costly product loss and prevent hazardous spills.
- Pulsation Dampeners - Removes virtually all hydraulic shock while producing a near steady flow of fluid. Protect piping, valves and fittings from destructive pulsations and surges. Available in a wide range of materials of construction
- Cycle Counter - The FTI Air Cycle Counter is an electronic device that counts pump cycles by detecting the presence of the valve carrier. The cycle counter can be universally used on any new or existing FTI Air pump with the proper air valve components.
- Liquid Level Control - The FTI Liquid Level Control is a pneumatic/mechanical device that will automatically turn the pump on and off as the liquid level changes
- Filter/Regulator - Compact, integrated design saves space and reduces piping, includes dual scale psi/Bar gage. Filters incoming air to five microns. Regulator adjusts air pressure from 7.3 to 120 psi (.5 to 8.3 bar).
- AODDampener - AODDampener is unique pulsation dampener manufactured from 316L stainless steel with PTFE backed diaphragm, has fully automatic air control and handles a wide variety of applications.
Putnam County Air-Operated Diaphragm Chemical Pump Designs & Their Advantages
Air Operated Diaphragm Chemical Pumps are a type of fluid-handling equipment that uses air pressure to move fluids. They come in different designs, such as single- and double-diaphragm models, ball valve designs, and nonmetallic wetted part constructions. These pumps are relatively affordable and versatile. They have high flow rates, can prime themselves, and can handle fluids that are abrasive or corrosive.
One key benefit is that they are self-priming and can run dry without damage, meaning they can be used even if the liquid levels fluctuate. Also, they can provide a steady flow rate with very little maintenance. Finally, since these pumps are air operated, they are easy to install and require minimal electricity usage.
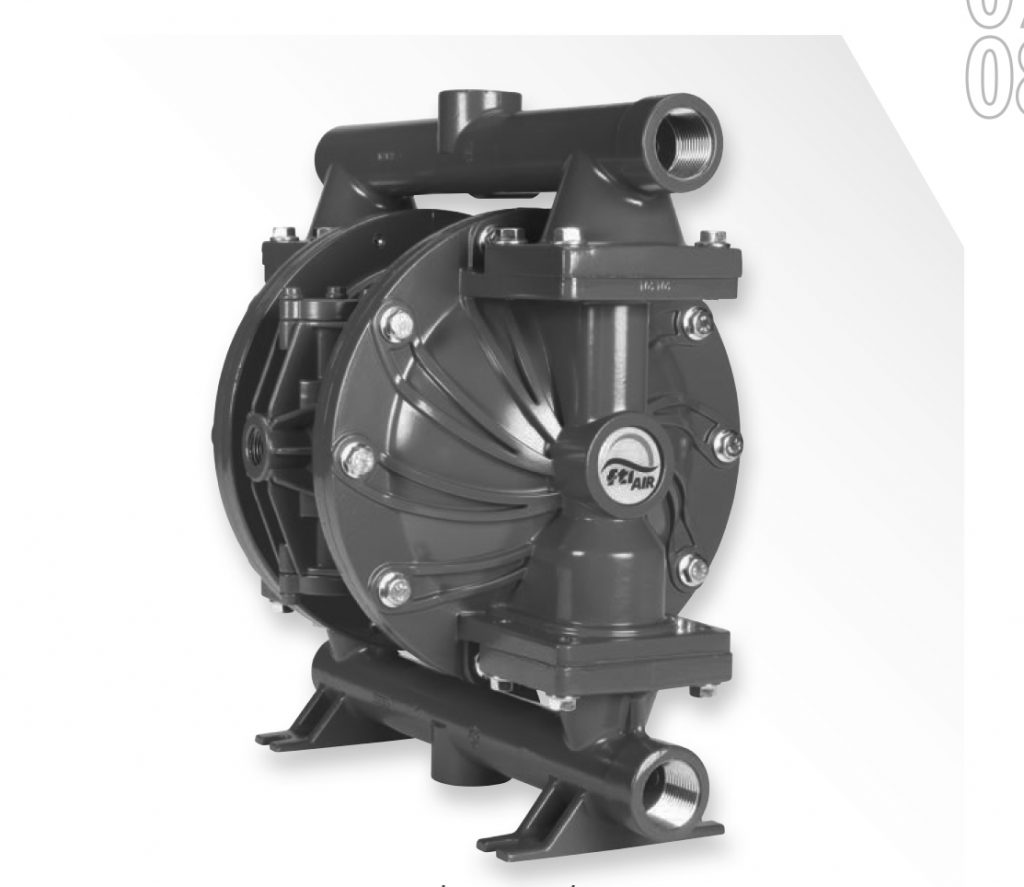
Putnam County Air-Operated Diaphragm Chemical Pumps and Their Applications
An Air Operated Diaphragm Chemical Pump is a type of positive displacement pump that uses a combination of compressed air and an elastic diaphragm to move chemical liquids. This type of pump is often used in industrial settings, such as chemical processing plants and water treatment facilities, due to its ability to handle high flow rates and corrosive materials. It’s also known for its superior design, as it can run dry without causing damage, making it more reliable than other types of pumps.
These pumps are highly versatile and have a wide range of applications. They are often used in the chemical, pharmaceutical, and food industries, as well as in industrial, agricultural, and water treatment operations. Air Operated Diaphragm Chemical Pumps can be used to transfer, meter, or dispense low to high-viscosity fluids and chemicals while providing precise, accurate flow rates with minimal maintenance.