
Industrial Chemical Pumps in Sullivan County
Sullivan County Small Centrifugal Pumps
Centrifugal pumps' high flow rates and capacity to handle large volumes of fluid are two of their main advantages. Additionally, they have a fairly simple design that is simple to maintain. Applications for Centrifugal pumps include water treatment, irrigation, oil & gas production, and chemical processing. Centrifugal pumps come in a variety of designs, including axial, mixed, and radial flow pumps. Each type has its own distinct set of qualities and is created for particular applications.
Sullivan County Small Centrifugal Pumps and How They Work
Centrifugal pumps use a rotating impeller to move fluid through a system. This impeller, which is a disk with vanes or blades attached to it, is driven by a motor and the rotation exerts a centrifugal force that causes the fluid to move away from the center of the disk. Due to the difference in pressure caused by this movement, the fluid is drawn into the pump and moved through the system. In addition to transferring fluids, these pumps can be utilized to transport gases.
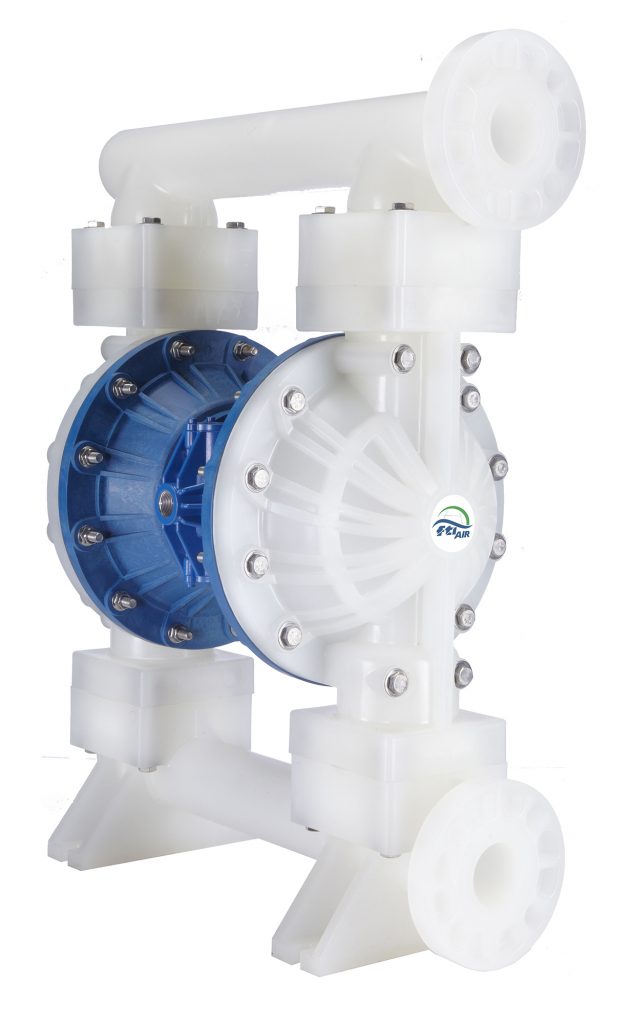
Sullivan County Air-Operated Diaphragm Chemical Pumps and Their Applications
An Air Operated Diaphragm Chemical Pump is a type of positive displacement pump that uses a combination of compressed air and an elastic diaphragm to move chemical liquids. This type of pump is often used in industrial settings, such as chemical processing plants and water treatment facilities, due to its ability to handle high flow rates and corrosive materials. It’s also known for its superior design, as it can run dry without causing damage, making it more reliable than other types of pumps.
These pumps are highly versatile and have a wide range of applications. They are often used in the chemical, pharmaceutical, and food industries, as well as in industrial, agricultural, and water treatment operations. Air Operated Diaphragm Chemical Pumps can be used to transfer, meter, or dispense low to high-viscosity fluids and chemicals while providing precise, accurate flow rates with minimal maintenance.
Sullivan County Drum Pump Accessories
- AODDampener - AODDampener is unique pulsation dampener manufactured from 316L stainless steel with PTFE backed diaphragm, has fully automatic air control and handles a wide variety of applications.
- Cycle Counter - The FTI Air Cycle Counter is an electronic device that counts pump cycles by detecting the presence of the valve carrier. The cycle counter can be universally used on any new or existing FTI Air pump with the proper air valve components.
- Pulsation Dampeners - Removes virtually all hydraulic shock while producing a near steady flow of fluid. Protect piping, valves and fittings from destructive pulsations and surges. Available in a wide range of materials of construction
- Liquid Level Control - The FTI Liquid Level Control is a pneumatic/mechanical device that will automatically turn the pump on and off as the liquid level changes
- Filter/Regulator - Compact, integrated design saves space and reduces piping, includes dual scale psi/Bar gage. Filters incoming air to five microns. Regulator adjusts air pressure from 7.3 to 120 psi (.5 to 8.3 bar).
- SPILLSTOP - Fully pneumatic system safely captures leaked product due to diaphragm failure and automatically shuts down failed pumps to eliminate costly product loss and prevent hazardous spills.
MSDB SERIES - MAGNETIC DRIVE, SEALLESS, Sullivan County CENTRIFUGAL PUMPS
- Compact close-coupled design
- High power neodymium magnetic drive system handles high specific gravity fluids
- Horizontal or vertical (with IEC motor only) installation
- Minimum flow rate is 1 gpm (.23m3/h)
- Engineered for corrosive fluids with polypropylene/Ryton© or PVDF/Ryton© construction
- Sealless design improves reliability with no seal maintenance to perform or seal leaks
- Two stage versions contain two impellers, three stage versions contain three impellers
- Heads up to 300 feet (91.5m)
- High specific gravity handling – over 1.8
- Maximum working pressure up to 135 PSI (9.3 bar)
Sullivan County Air-Operated Diaphragm Chemical Pump Designs & Their Advantages
Fluid-handling devices that employ air pressure to transfer fluids include air operated diaphragm chemical pumps. They are available in several designs, including single- and double-diaphragm models, ball valve layouts, and nonmetallic wetted component setups. These pumps are adaptable and reasonably priced. They can tolerate caustic or abrasive fluids, have high flow rates, and can prime themselves.
They can be used even if the liquid levels change because they are self-priming and can run dry without causing damage. Additionally, they require relatively little maintenance and can deliver a constant flow rate. Last but not least, because these pumps are air-operated, they are simple to install and use a small amount of electricity.